Choosing the Right Production Line Based on Daily Output Requirements
Oct.07, 2026
Choosing the Right Production Line Based on Daily Output Requirements starts with converting demand into a realistic saleable-output target. I evaluate daily orders, takt time, cycle time, uptime, yield, changeovers, product variety, factory space, labor availability, automation level, and planned growth before selecting equipment. A line rated for 1,000 units per shift may produce fewer saleable units after stoppages, setup changes, quality losses, and bottleneck constraints.
For manufacturers, the most reliable approach is to calculate required capacity first, then compare production-line layouts and automation levels against that requirement. This article explains how I assess line capacity, select equipment for low, medium, and high daily output, identify the bottleneck, calculate total cost, and validate a supplier before purchasing.
!
Key Takeaways
- Required saleable output depends on takt time, cycle time, uptime, yield, changeovers, and bottleneck capacity.
- Low-volume manufacturers often benefit from flexible or semi-automatic lines before investing in full automation.
- High-volume LPG cylinder production requires balanced stations, controlled material flow, testing capacity, and maintenance planning.
- A supplier should demonstrate run rates, acceptance-test results, quality data, service response, and upgrade options.
- Total ownership cost includes labor, utilities, maintenance, integration, training, downtime risk, and future expansion.
- Shuofang provides automated, semi-automated, and segmented LPG cylinder production-line configurations for different capacity requirements.
Start With Production Capacity Planning
Production capacity planning means matching the equipment’s realistic output with the number of saleable products required during a defined period. I begin with daily demand rather than the supplier’s maximum machine speed because nominal speed usually excludes breaks, material handling, quality checks, changeovers, maintenance, and rejected products.
The basic capacity model is:
Saleable daily output = operating time × cycle rate × uptime × yield − changeover losses
If several stations operate in sequence, the capacity of the entire line is controlled by the slowest effective station. For example, a forming machine may process 80 cylinders per hour, while circumferential welding handles only 60 cylinders per hour. In that case, the line cannot consistently sell 80 cylinders per hour unless the welding stage is upgraded, duplicated, or supported by an appropriate buffer.
I also separate three capacity levels:
| Capacity level | Typical planning condition | Suitable production approach |
|---|---|---|
| Low daily output | Variable demand, limited product range, fewer than 300 units per day | Manual or semi-automatic equipment |
| Medium daily output | Stable demand, repeated products, approximately 300–1,000 units per day | Semi-automatic or mixed automation |
| High daily output | Contract production, stable orders, more than 1,000 units per day | Fully automated or parallel-station line |
These thresholds are planning references rather than universal limits. The correct range depends on cylinder size, wall thickness, process route, shift length, inspection requirements, and the number of product variants. I would confirm the figures through a supplier’s tested production data before finalizing the purchase.
Calculate Takt Time and Required Production Speed
Takt time shows how frequently a finished product must leave the line to meet customer demand. I calculate it using:
Takt time = available production time ÷ required daily output
Suppose a plant operates one 8-hour shift, with 30 minutes for breaks and 30 minutes for planned cleaning. The net available time is 7 hours, or 25,200 seconds. If the required output is 600 saleable LPG cylinders per day, the takt time is:
25,200 seconds ÷ 600 cylinders = 42 seconds per cylinder
The line must therefore complete one saleable cylinder every 42 seconds on average. A station with a 50-second cycle time becomes a capacity constraint unless the process is redesigned, the station is duplicated, or the daily target is reduced.
I then adjust the calculation for real operating conditions. Assume the line has:
- 42-second takt time
- 38-second nominal cycle time
- 85% uptime
- 98% first-pass yield
- 30 minutes of changeover loss
- 7 hours of scheduled production time
The effective output is approximately:
25,200 seconds − 1,800 seconds changeover = 23,400 seconds
The theoretical cycle output is:
23,400 ÷ 38 = 615 units
After applying 85% uptime and 98% yield:
615 × 0.85 × 0.98 = approximately 512 saleable units per day
This result is below the 600-unit requirement, even though the nominal cycle rate initially appeared sufficient. I would respond by reducing changeover time, increasing uptime, lowering the bottleneck cycle time, adding a parallel station, or selecting a line with additional capacity.
Match the Line Type to Product Complexity and Variety
The physical production line should reflect the product family, manufacturing process, and number of variations. A single-product line can use dedicated fixtures and automatic feeding systems, while a multi-product plant needs adjustable tooling, recipe management, flexible handling, and shorter changeovers.
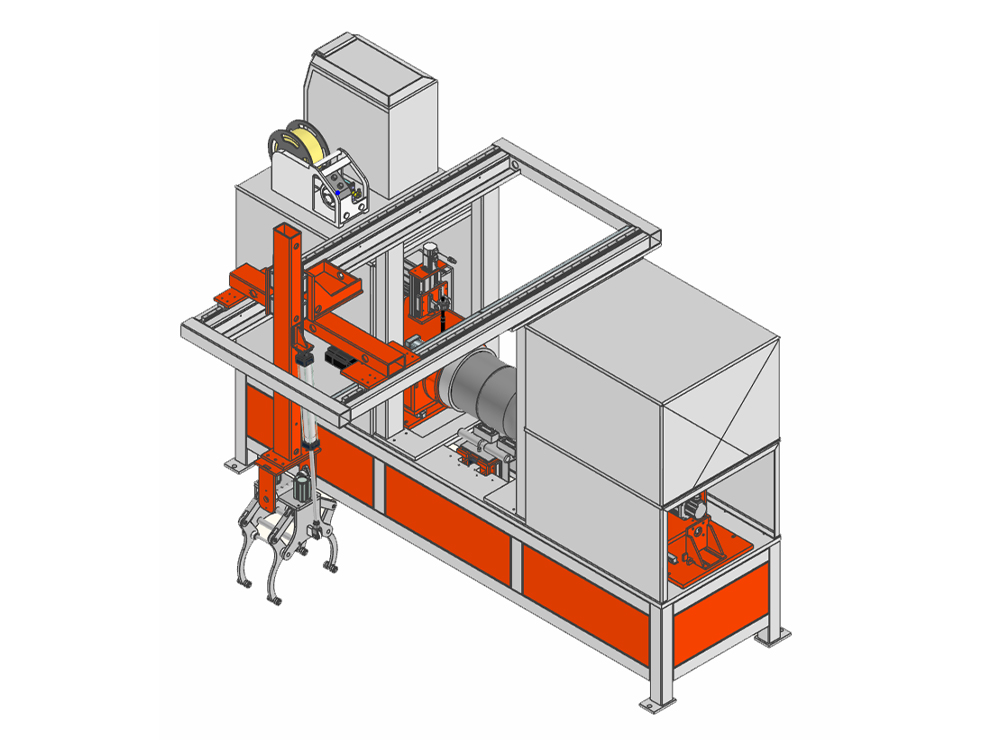
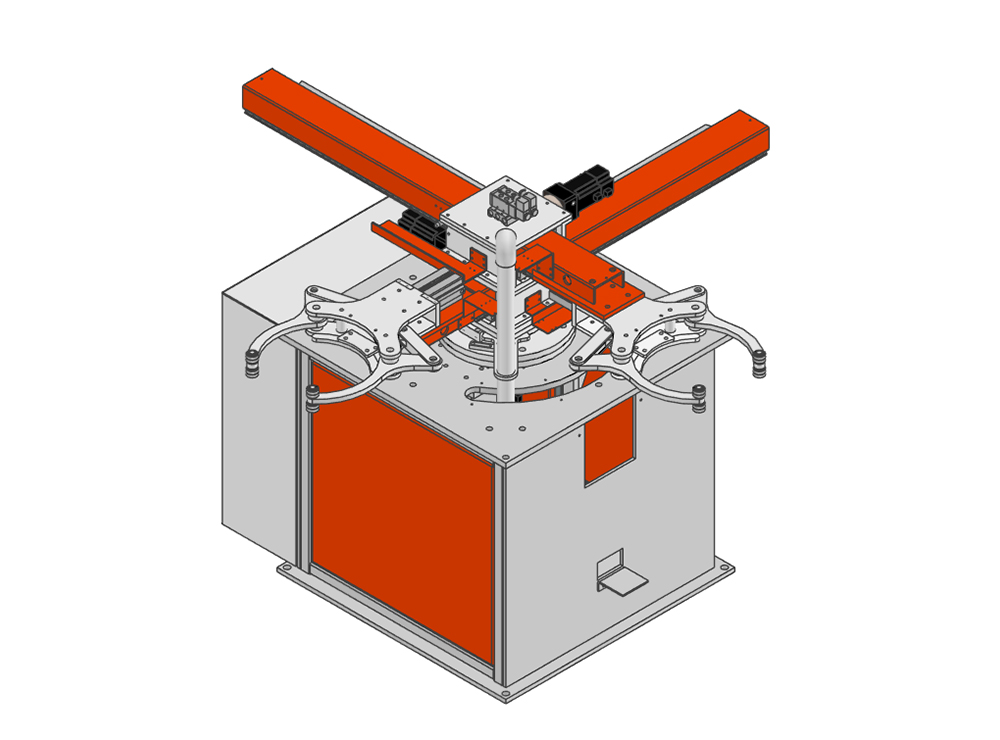
For LPG cylinder manufacturing, the process may include material preparation, deep drawing, trimming, valve-seat welding, handle and base welding, circumferential welding, heat treatment, surface coating, valve mounting, hydrostatic testing, air leakage testing, and marking. I would map each process before reviewing equipment because adding automation to one stage does not solve a capacity problem in another stage.
A linear layout is suitable when the process sequence is stable and material moves in one direction. A U-shaped layout can reduce operator walking and support compact supervision when the line includes manual loading or inspection. A segmented layout is useful when the manufacturer wants to automate only selected processes, such as welding, testing, or coating, while retaining manual handling in lower-volume areas.
Product variety also changes the investment decision. If the plant produces 6 kg, 12.5 kg, and 15 kg cylinders, I would request changeover times, tooling requirements, recipe controls, and trial results for every size. A line that performs well on one cylinder specification may require different fixtures, welding parameters, or testing settings for another.
Compare Manual, Semi-Automatic, and Fully Automated Production Lines
Automation should be selected according to daily output, labor cost, quality requirements, and the stability of demand. I do not treat full automation as automatically superior because an oversized system can increase integration costs, training requirements, maintenance complexity, and financial exposure.
Manual production lines
Manual equipment may fit small manufacturers with low daily output, many product variations, or uncertain demand. The initial equipment cost is usually lower, and operators can adjust quickly when specifications change. However, manual handling can create greater variation in welding position, material transfer, inspection consistency, and labor productivity.
Semi-automatic production lines
Semi-automatic equipment combines operator loading or transfer with automated forming, welding, testing, or coating functions. This arrangement is often suitable for growing manufacturers that need better repeatability but cannot justify a complete automated system.
I would consider semi-automatic production when daily output is approximately 300–1,000 units, demand is increasing, and the company needs a staged investment path. The purchase specification should include operator count per shift, expected cycle time, changeover procedure, fixture life, and the possibility of adding automated handling later.
Fully automated production lines
Fully automated lines are generally appropriate when demand is stable, product specifications are standardized, and the required output is high enough to support the investment. Robots, automatic feeding, sensors, programmable controls, in-line inspection, and production monitoring can reduce manual transfer and improve process consistency.
Automation also requires suitable infrastructure. I check compressed-air capacity, electrical load, floor loading, ventilation, safety guarding, material storage, maintenance access, and space for finished-goods handling. A line that fits the production process but cannot fit the building or utility system is not a practical solution.
Control Bottlenecks, Buffers, and Line Balance
The bottleneck station determines the maximum sustained output of a production line. I identify it by comparing the effective cycle time of every major operation, including loading, processing, inspection, unloading, and internal transfer.
For example:
| Station | Effective cycle time | Approximate hourly capacity |
|---|---|---|
| Deep drawing | 32 seconds | 112 units |
| Trimming and joggling | 35 seconds | 103 units |
| Valve-seat welding | 42 seconds | 86 units |
| Circumferential welding | 48 seconds | 75 units |
| Hydro testing | 40 seconds | 90 units |
| Air leakage testing | 36 seconds | 100 units |
The circumferential welding station limits the line to approximately 75 units per hour before uptime and yield adjustments. Adding a faster deep-drawing machine would not increase saleable output unless the welding constraint is addressed.
I use three common methods to improve balance. First, I reduce the bottleneck cycle time through tooling, parameter adjustment, or automation. Second, I add a parallel station when the process can be divided without reducing quality control. Third, I place a controlled buffer before the bottleneck to prevent short upstream interruptions from starving the constrained process.
Buffers must be sized carefully. A large buffer can hide recurring problems and increase work-in-process inventory, while a small buffer may not protect the bottleneck from normal variation. The correct size depends on failure frequency, repair time, changeover duration, and the safety requirements of the process.
Add Sensors, MES, and Digital Production Monitoring
Modern production-line selection should include the control and data layer, not only mechanical equipment. Sensors can track temperature, pressure, welding current, position, vibration, cycle time, and equipment status. These measurements help maintenance teams identify deviations before they become repeated defects or extended downtime.
A manufacturing execution system, or MES, can connect work orders with production status, operator actions, quality results, downtime codes, and traceability records. For LPG cylinder production, I would prioritize data collection for welding parameters, heat-treatment conditions, hydrostatic testing, air leakage testing, marking, and final inspection.
Digital twins can be useful when the line is complex or expansion plans are uncertain. A simulation model can test material flow, buffer sizes, station utilization, robot reach, operator access, and the effect of adding a second bottleneck station. I would use a digital model before construction when the facility has limited space or when the planned output requires multiple shifts.
The key metric is not the number of sensors installed. It is whether the data supports specific decisions, such as reducing unplanned downtime, identifying the reason for rejected cylinders, improving changeover time, or calculating OEE accurately.
Evaluate Quality, Maintenance, and Downtime Risk
Capacity without quality is not saleable production. I therefore evaluate inspection capacity together with forming and welding capacity. A line may produce 1,000 units per day, but if testing can process only 700 units or if the reject rate reaches 5%, the practical saleable output is lower.
For LPG cylinder production, the equipment plan may include hydro testing machines, air leakage testing machines, welding inspection, heat-treatment controls, coating inspection, and traceable final checks. The acceptance criteria should define pressure-test performance, leak-test results, dimensional tolerances, weld appearance, coating coverage, and documentation requirements according to the applicable market standard.
Maintenance planning should cover spare parts, lubrication points, preventive-maintenance intervals, troubleshooting procedures, and technician training. I would request the mean time to repair for common faults, the recommended critical spares list, remote diagnostic capability, and the supplier’s service response target.
Shuofang states that its equipment includes a one-year warranty, free replacement of parts during the warranty period, and lifetime technical support. The company also describes installation, commissioning, operator training, and operation guidance for overseas projects. I would still place these commitments in the purchase contract with defined response times, included services, exclusions, and escalation procedures.
Use a Total-Cost Decision Model
The purchase price is only one part of production-line investment. I compare total cost over the planned operating period using the following structure:
Total cost of ownership = equipment price + installation + integration + utilities + labor + maintenance + training + downtime risk + expansion cost
For example, a fully automated line may reduce operators per shift but require more controls engineering, spare parts, software support, and specialized maintenance. A semi-automatic line may require additional labor but offer lower integration cost and easier product changeovers.
I would collect these figures before comparing suppliers:
- Number of operators per shift
- Electricity, compressed-air, gas, and water consumption
- Expected uptime and maintenance hours
- Spare-parts cost for 12 months
- Training and commissioning duration
- Floor-space and building-modification cost
- Cost of rejected products and rework
- Estimated cost of adding capacity later
- Expected production loss during installation
Return on investment should be based on saleable output, not nominal machine speed. If a line produces 500 saleable cylinders per day instead of its advertised 600-unit nominal rate, the revenue model must use 500. This approach produces a more realistic payback calculation and reduces the risk of selecting equipment that appears inexpensive but cannot meet the required demand.
Validate the Supplier Before Signing
I use a structured supplier-validation process rather than relying only on brochures. First, I request demonstrated run rates using the same product dimensions, materials, tooling, and quality requirements planned for the factory. The trial should record cycle time, uptime, yield, changeover duration, labor requirements, and energy consumption.
Second, I require a factory acceptance test and a site acceptance test. The acceptance document should define the target output, minimum uptime, maximum reject rate, test procedures, safety functions, documentation, and the process for correcting failed results.
Third, I review the supplier’s service system. Shuofang describes Henan Shuofang Intelligent Equipment Co., Ltd. as an LPG cylinder production-line supplier with more than 10 years of industry focus, a production base exceeding 20,000 square meters, and annual output value above 70 million yuan. The company also presents automated, semi-automated, and segmented production-line solutions, along with case information for a project producing 1.68 million LPG cylinders annually.
I would verify each claim through current project records, customer references, production data, and an on-site demonstration. I would also ask whether the supplier can upgrade the line later with additional welding stations, automatic material handling, sensors, testing equipment, MES functions, or expanded tooling. Upgrade capability is particularly important for small manufacturers that expect output to increase in stages.
How to Choose the Right Production Line Based on Daily Output Requirements
The selection process should follow a clear sequence:
- Define saleable daily demand. Use confirmed orders, forecast demand, safety stock, and seasonal variation rather than a single optimistic target.
- Calculate takt time. Divide net available production time by required daily output.
- Measure the full process route. Include forming, welding, treatment, coating, testing, inspection, handling, and packaging.
- Identify the bottleneck. Use effective cycle time after uptime, changeovers, and quality losses.
- Select the automation level. Match manual, semi-automatic, or fully automated equipment to demand stability, labor availability, and capital limits.
- Check the factory layout. Confirm material flow, safety clearance, utility capacity, maintenance access, and expansion space.
- Model total ownership cost. Include labor, utilities, integration, training, maintenance, downtime, and future upgrades.
- Validate the supplier. Require run-rate demonstrations, acceptance testing, quality records, service commitments, and upgrade plans.
This process prevents a common purchasing error: choosing a line from its maximum rated speed without checking whether the complete system can deliver the required number of saleable products every day.
Final Considerations
Choosing the Right Production Line Based on Daily Output Requirements requires more than comparing machine speeds or selecting the largest available system. I would begin with saleable demand, calculate takt time, adjust for uptime and yield, identify the bottleneck, and then compare line layouts and automation levels against the actual production environment.
For low daily output, flexible or semi-automatic equipment may control financial risk and support product variety. For medium output, balanced stations and staged automation can provide a practical path for expansion. For high daily output, I would prioritize automated material flow, parallel bottleneck stations, testing capacity, MES monitoring, preventive maintenance, and supplier-backed acceptance testing.
Shuofang’s lpg cylinder production line options may be relevant for manufacturers comparing automated, semi-automated, and segmented configurations. Before purchasing, I would provide the supplier with cylinder specifications, required daily output, shift pattern, product mix, factory layout, utility conditions, quality standards, and expansion plans. The final decision should be based on demonstrated saleable capacity, total cost of ownership, maintenance support, and the line’s ability to meet future demand without requiring a complete replacement.